Precision modular batch refining engineered in Uttar Pradesh to convert UCO, Non-Edible Oils and Fats into high-cetane, BIS IS 15607:2022 compliant Biodiesel (B100) for Oil Marketing Companies and institutional energy partners.
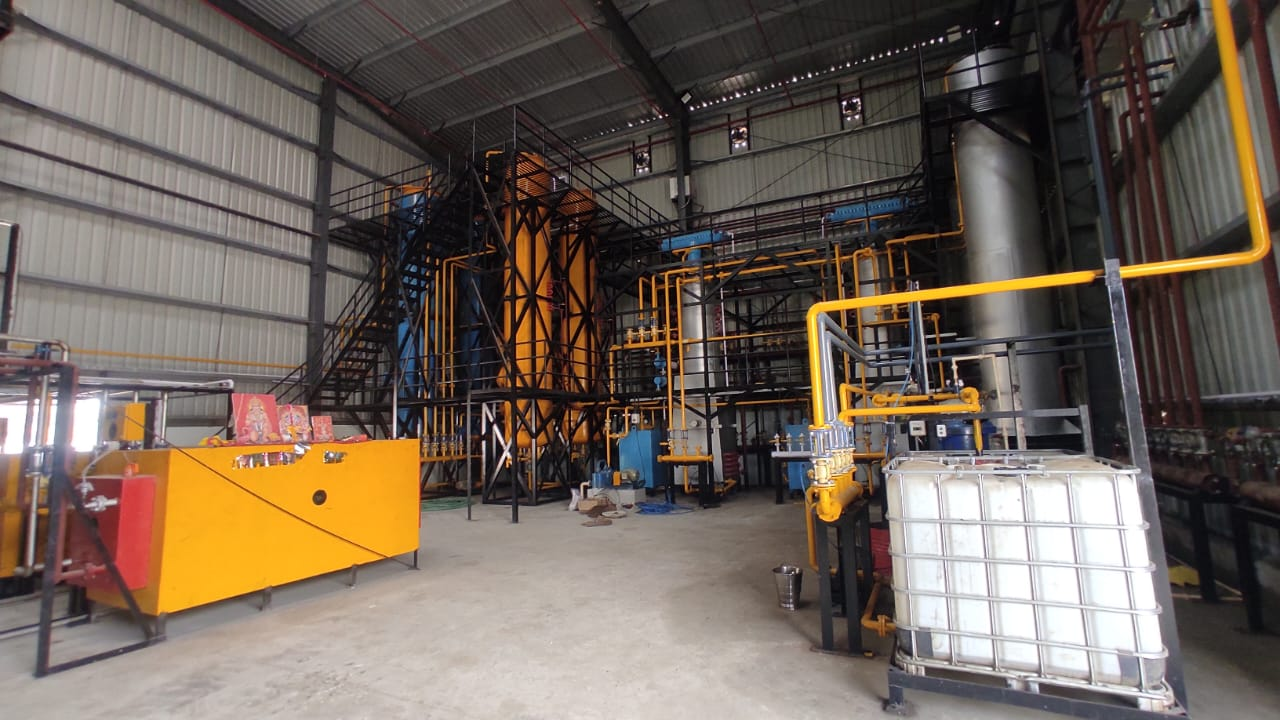
Bigfuel Nxtgen India Private Limited operates a dedicated 30 KLPD modular batch process refining facility at Vill.- Bharawan, Sandila, Hardoi, Uttar Pradesh, India.
Designed for multi-feedstock versatility, our plant efficiently converts UCO, Non-Edible Oils and Fats into high-purity Biodiesel (B100) for Oil Marketing Companies (OMCs) and bulk industrial consumers, while recovering valuable oleochemical co-products.
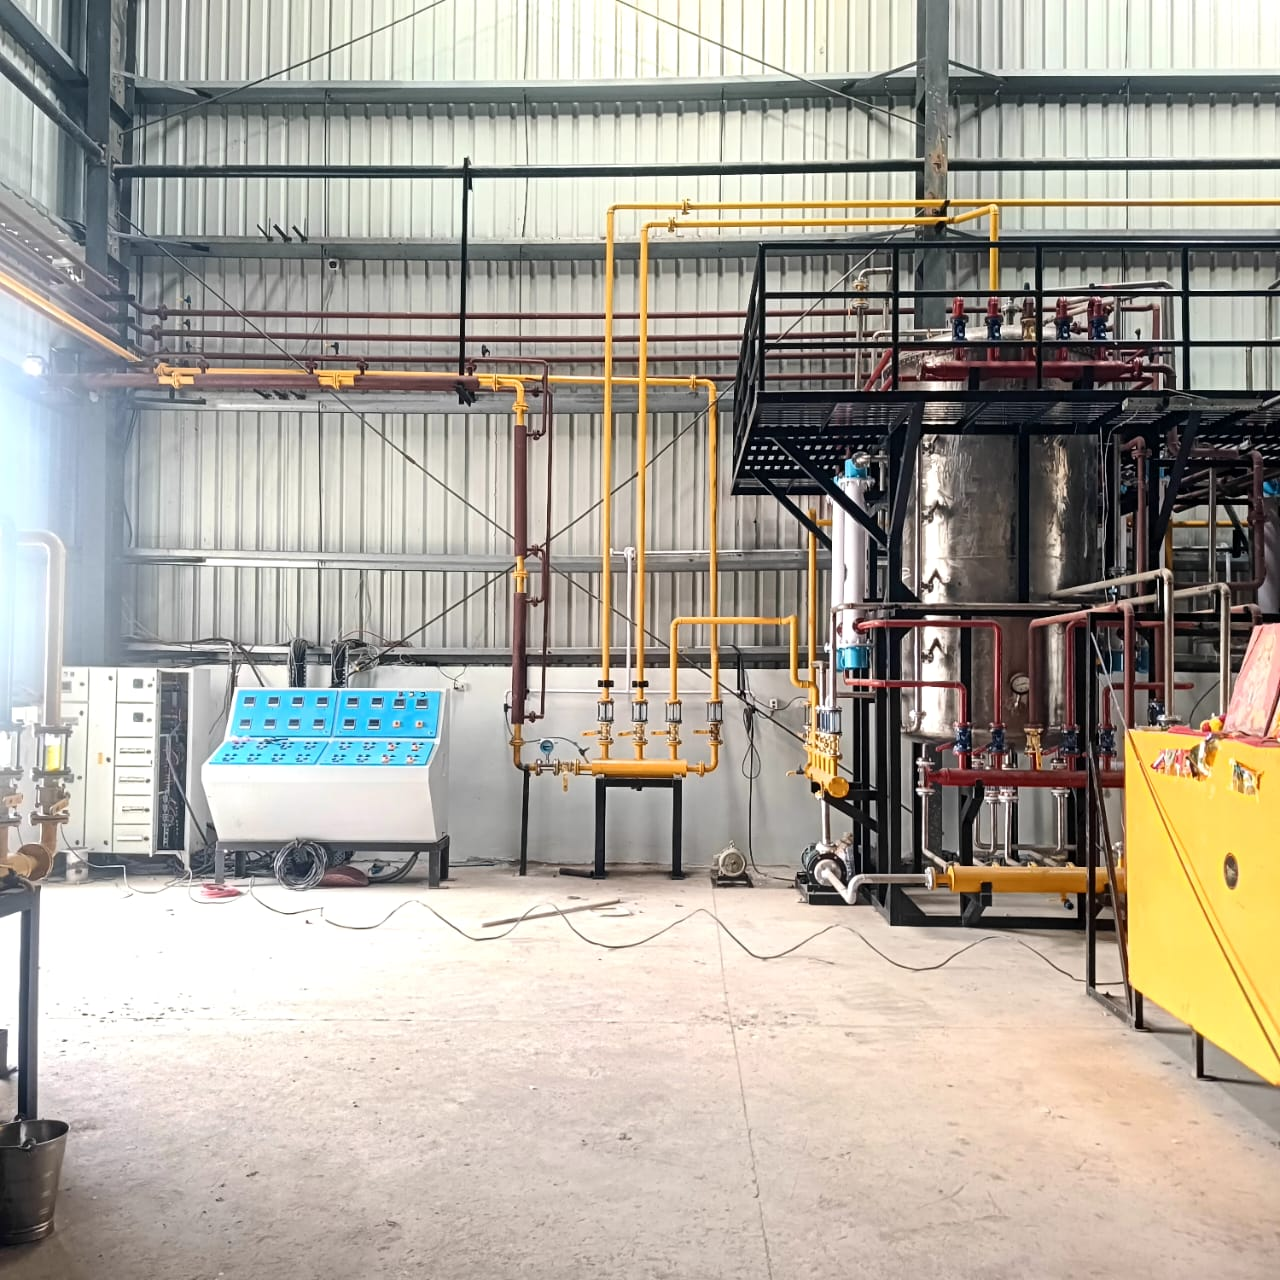
Main Processing Reactor & Automated Control Console
Approved under the Uttar Pradesh Bio-Energy Policy 2022 (Project Code: 119 BG493), advancing indigenous clean-fuel manufacturing and national biodiesel blending goals.
Our 30 KLPD modular batch process refining architecture integrates five core purification and conversion technologies for batch-to-batch consistency:
Self-reliant industrial utilities installed across our Vill.- Bharawan, Sandila, Hardoi campus to guarantee uninterrupted 30 KLPD operations and verified dispatch accuracy.
Clean captive renewable power generation integrated into the factory grid, reducing auxiliary carbon intensity across daily refining and laboratory operations.
Automated voltage stabilization and Automatic Power Factor Correction (APFC) protecting sensitive PLC consoles, motors, and analytical instruments.
Uninterrupted industrial backup power ensuring zero thermal disruption during batch transesterification, vacuum dehydration, and centrifuge cycles.
Segregated feedstock, intermediate ester, methanol, and finished B100 storage tanks with dedicated transfer manifolds and fire-hydrant protection.
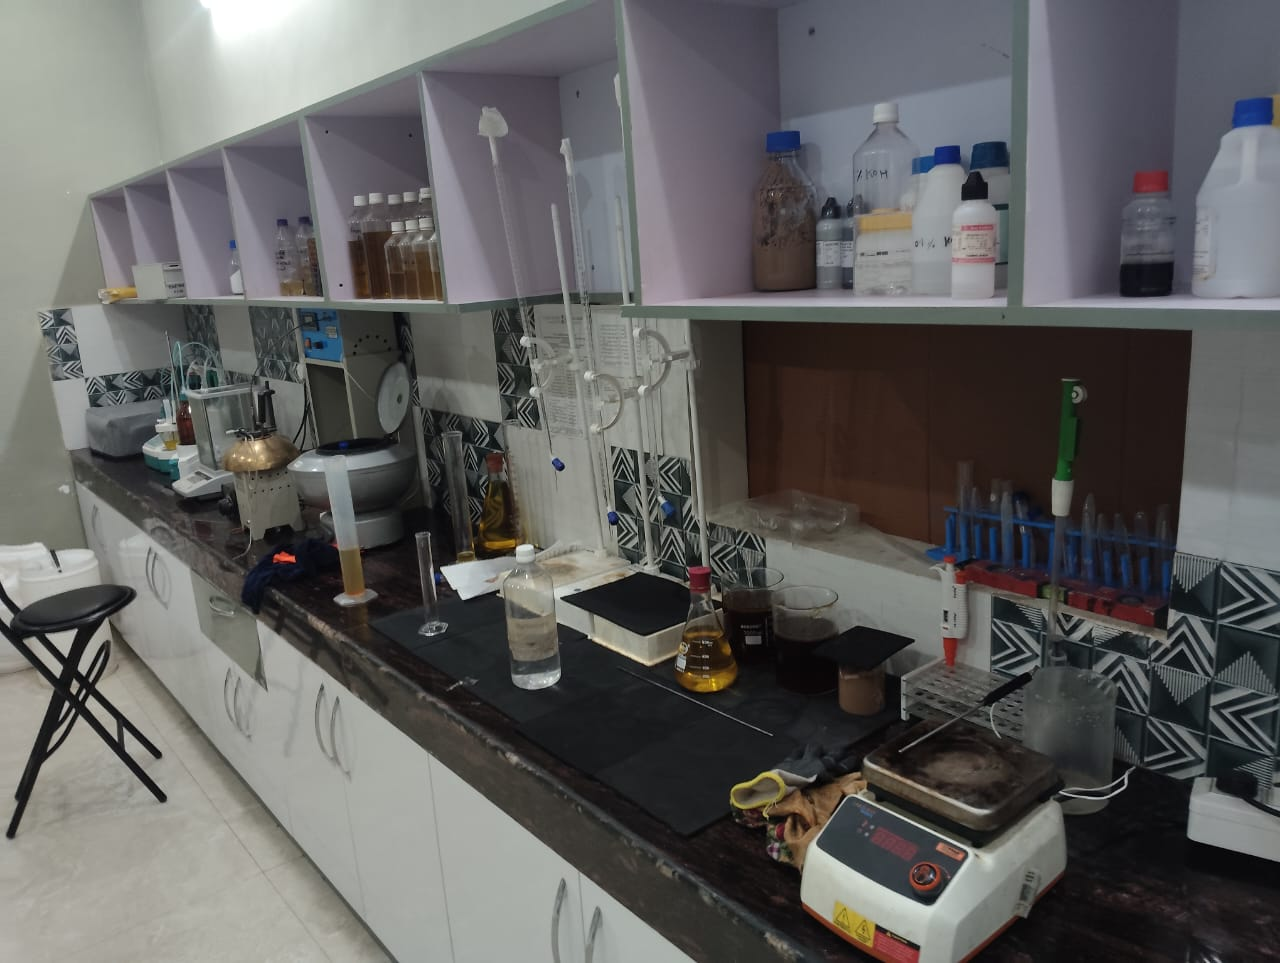
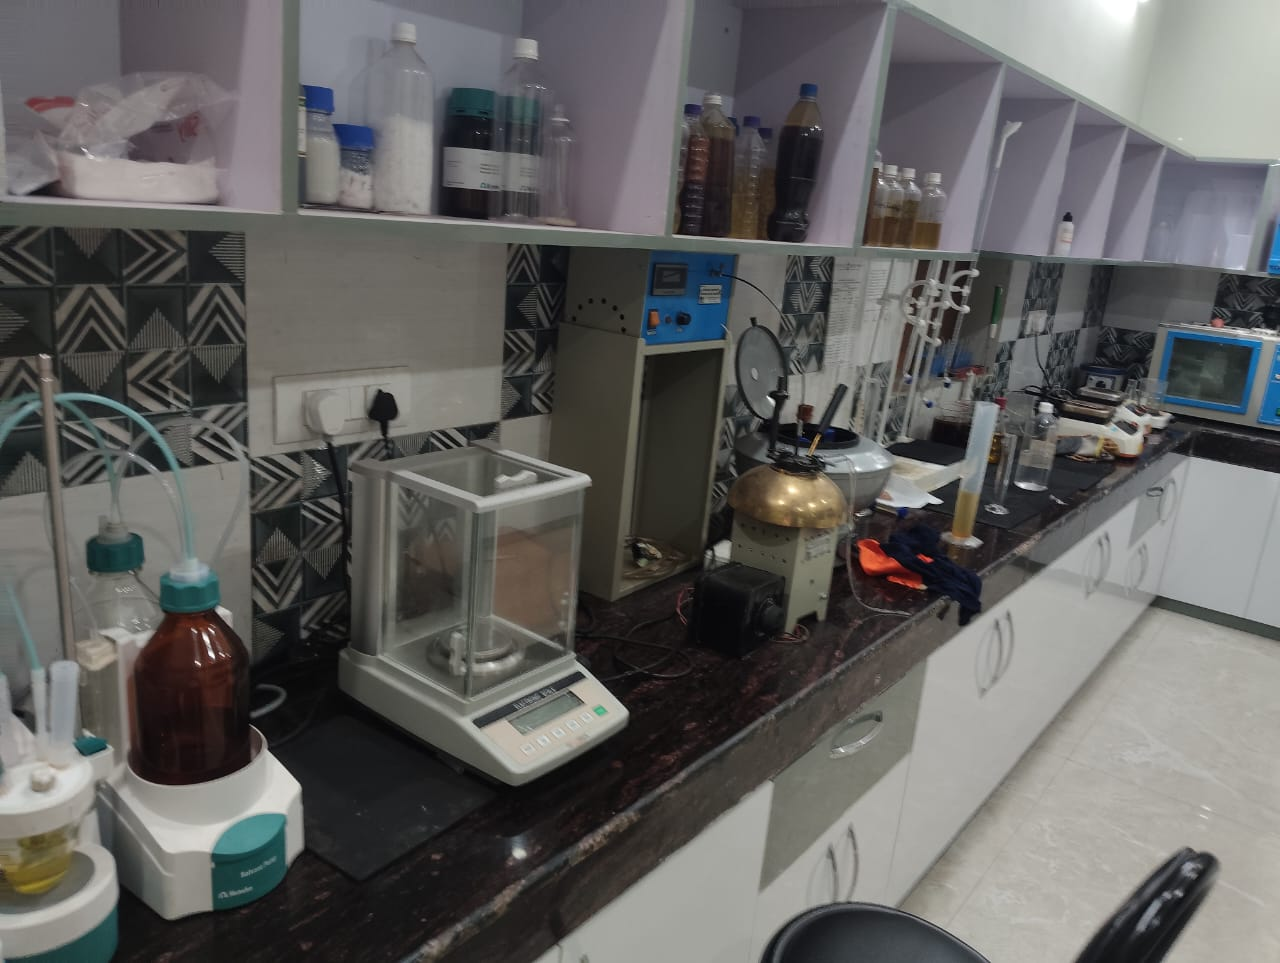
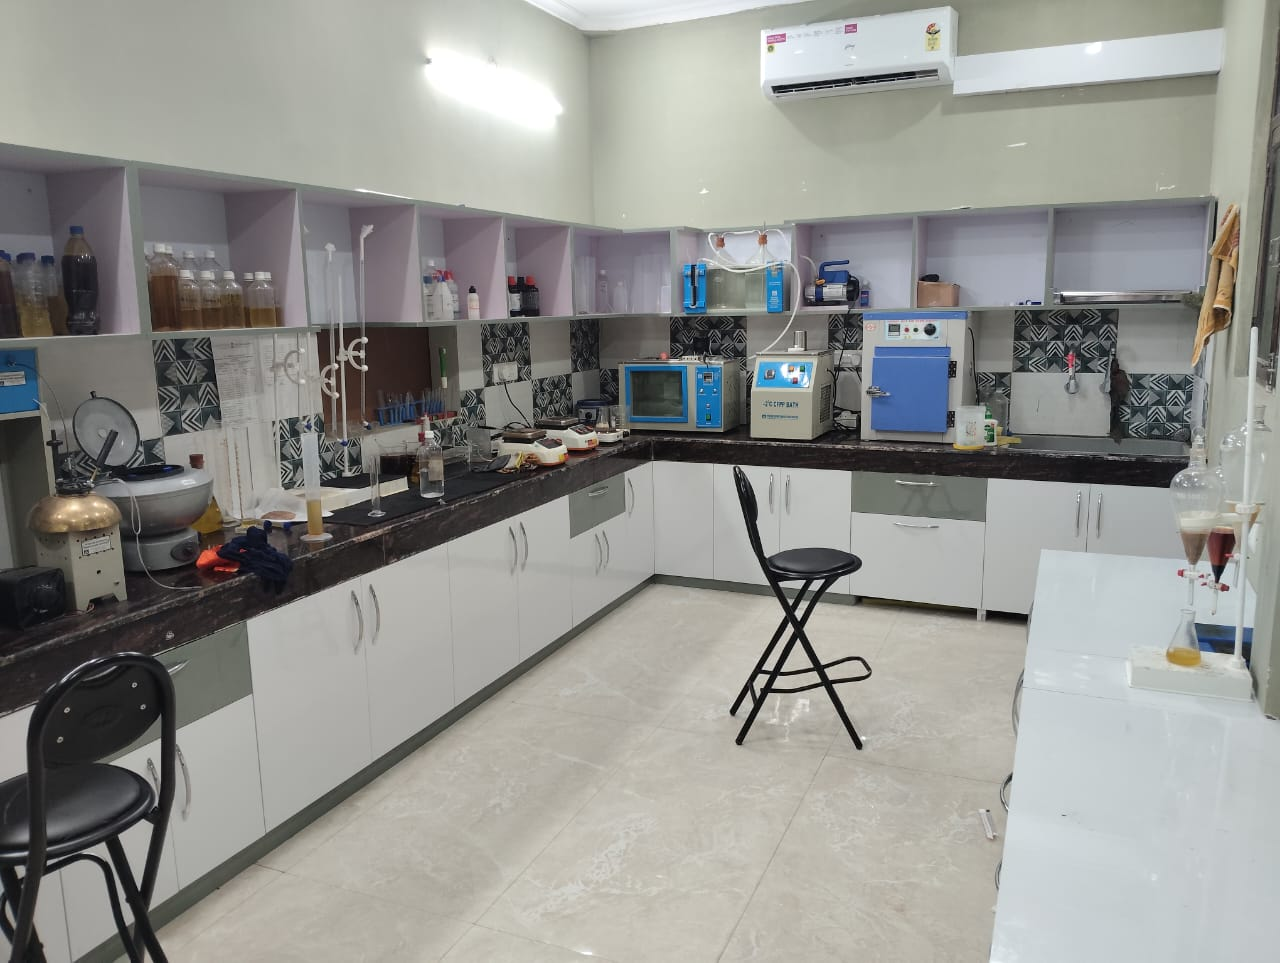
Comprehensive pre-dispatch BIS IS 15607:2022 testing equipped with precision analytical balances, titration stations, flash point tester, CFPP bath, and vacuum oven.
Precision raw material intake and bulk OMC tanker dispatch weighment on campus for transparent, audit-ready material accounting.
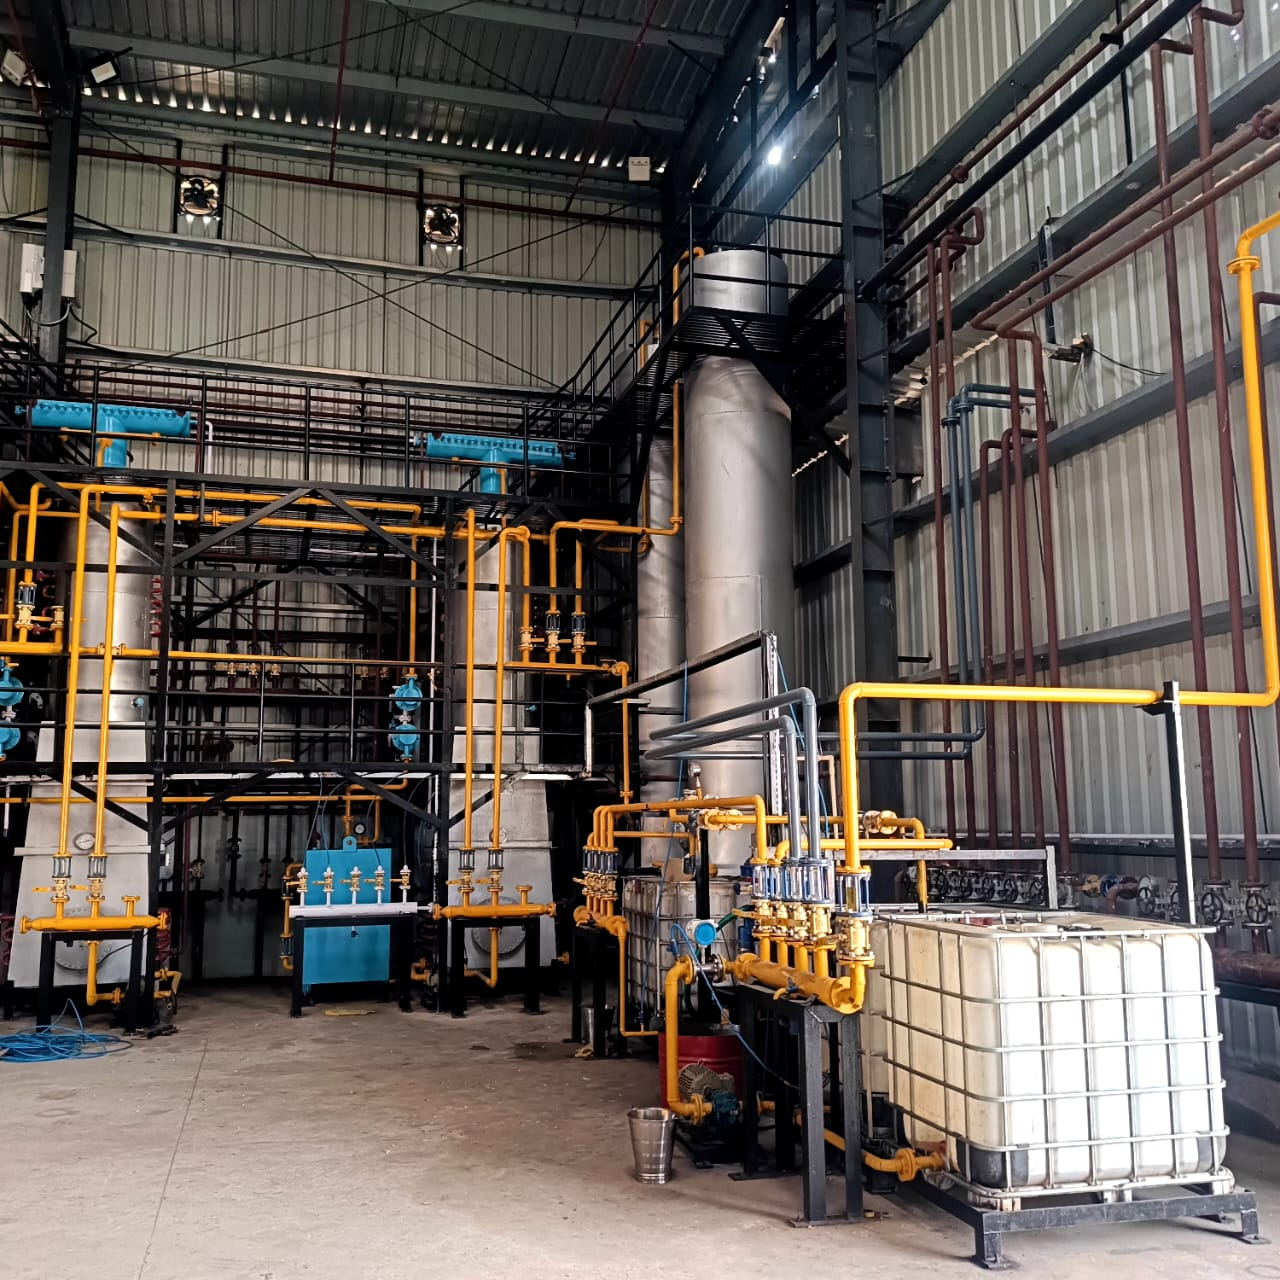
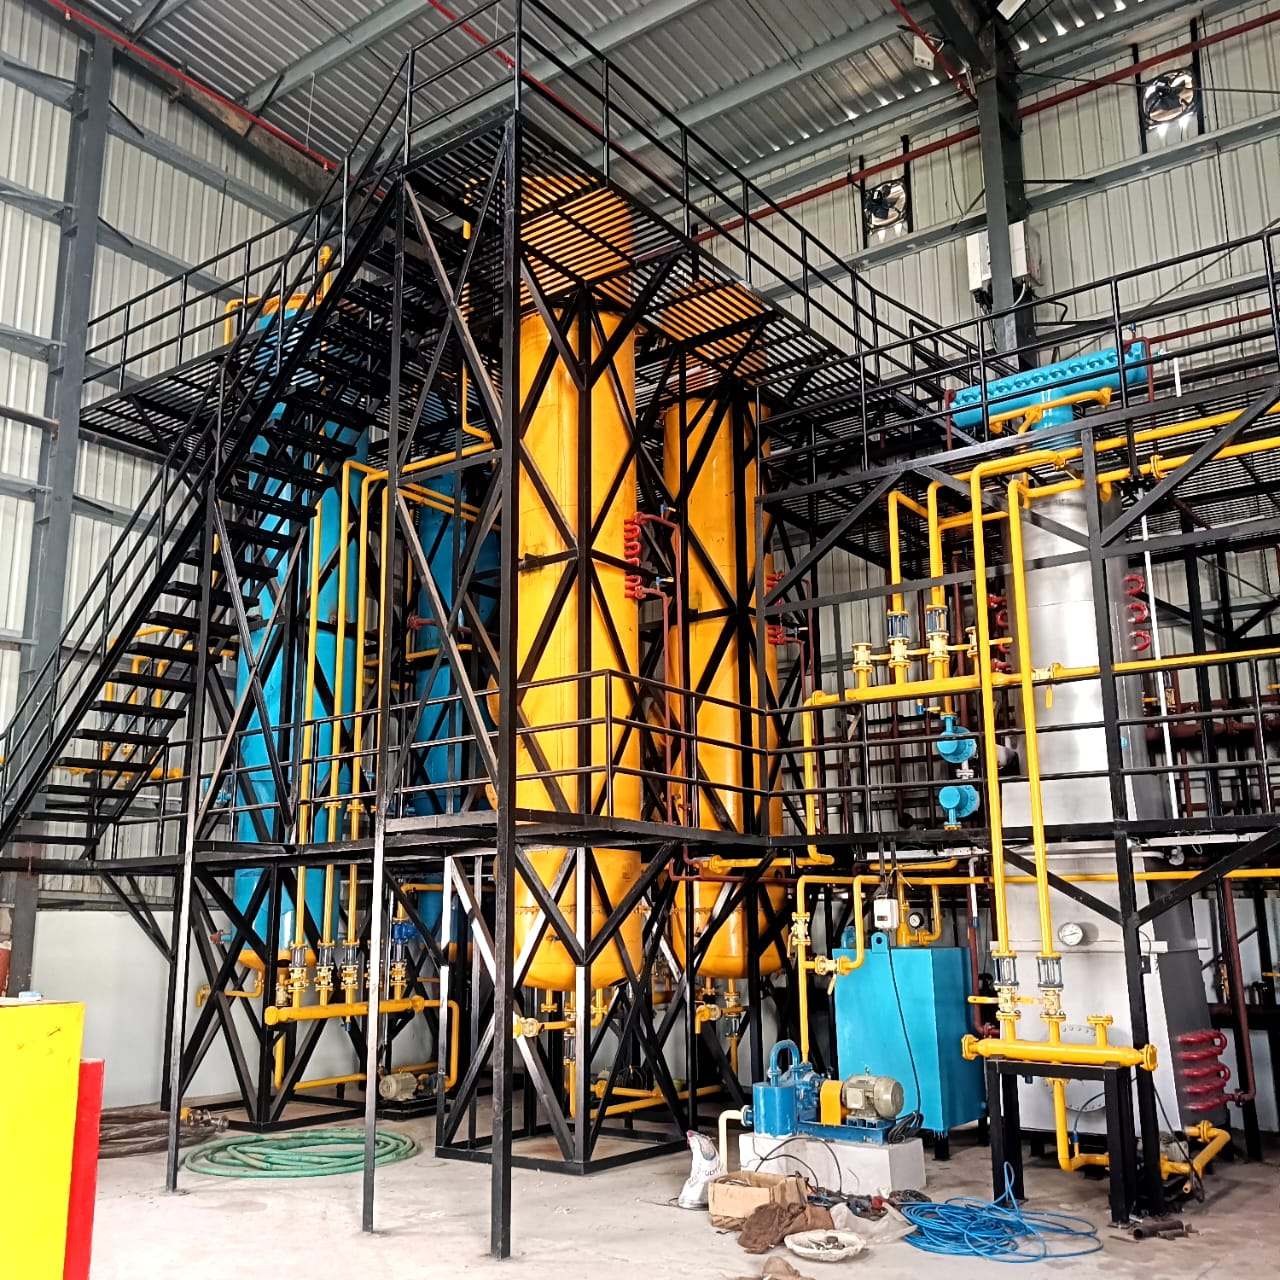
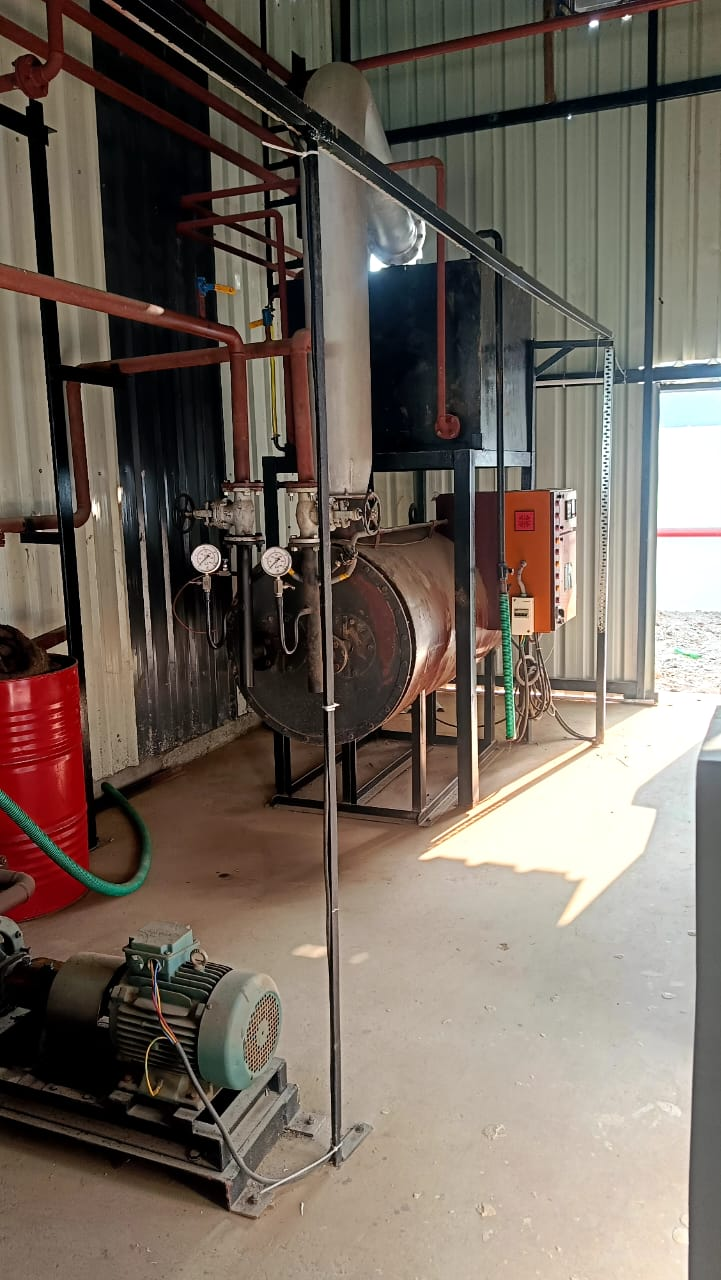
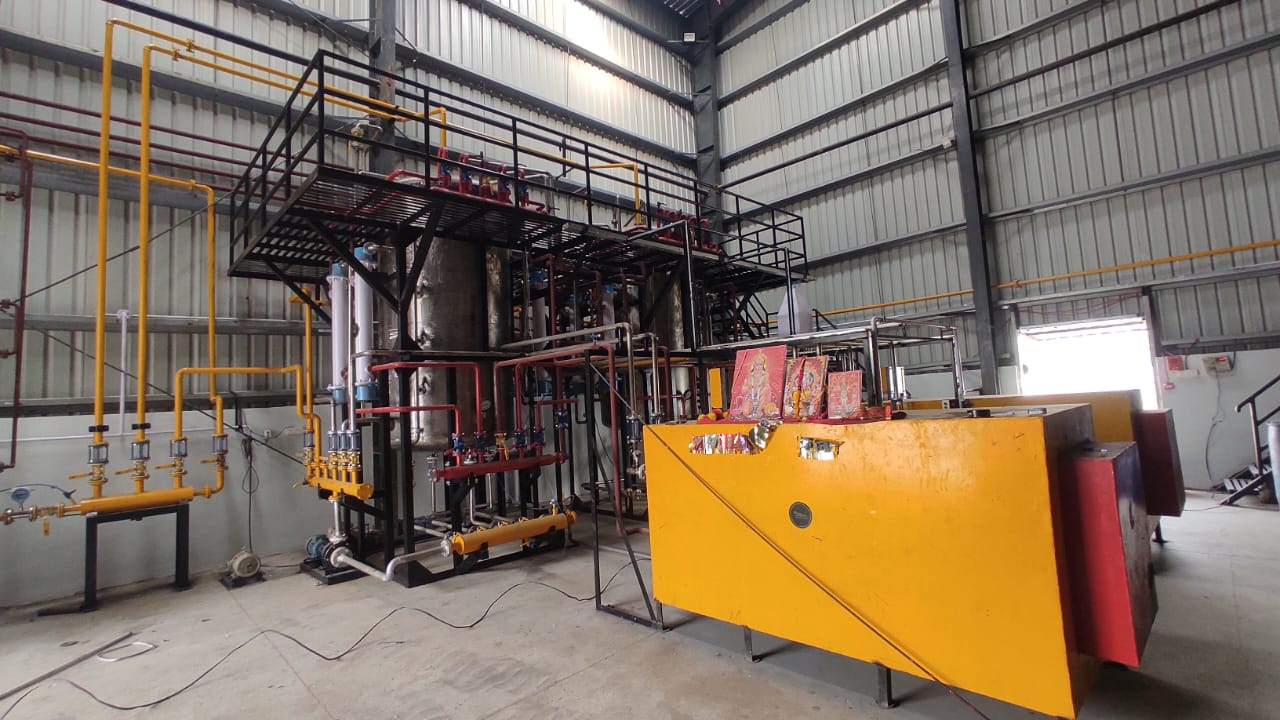
Explore our actual processing reactors, distillation columns, utility systems, and analytical wet chemistry laboratory at Vill.- Bharawan, Sandila, Hardoi.
Integrated 30 KLPD facility with rooftop solar, 450 KL storage tank farm, and 60T weighbridge at Vill.- Bharawan, Sandila, Hardoi.
Centralized process instrumentation & stainless reactor bay.
Heavy-duty modular batch processing skid and valving.
High-capacity vertical purification and separation columns.
Closed-loop solvent rectification & precision flow manifold.
Controlled thermal energy delivery for esterification reactions.
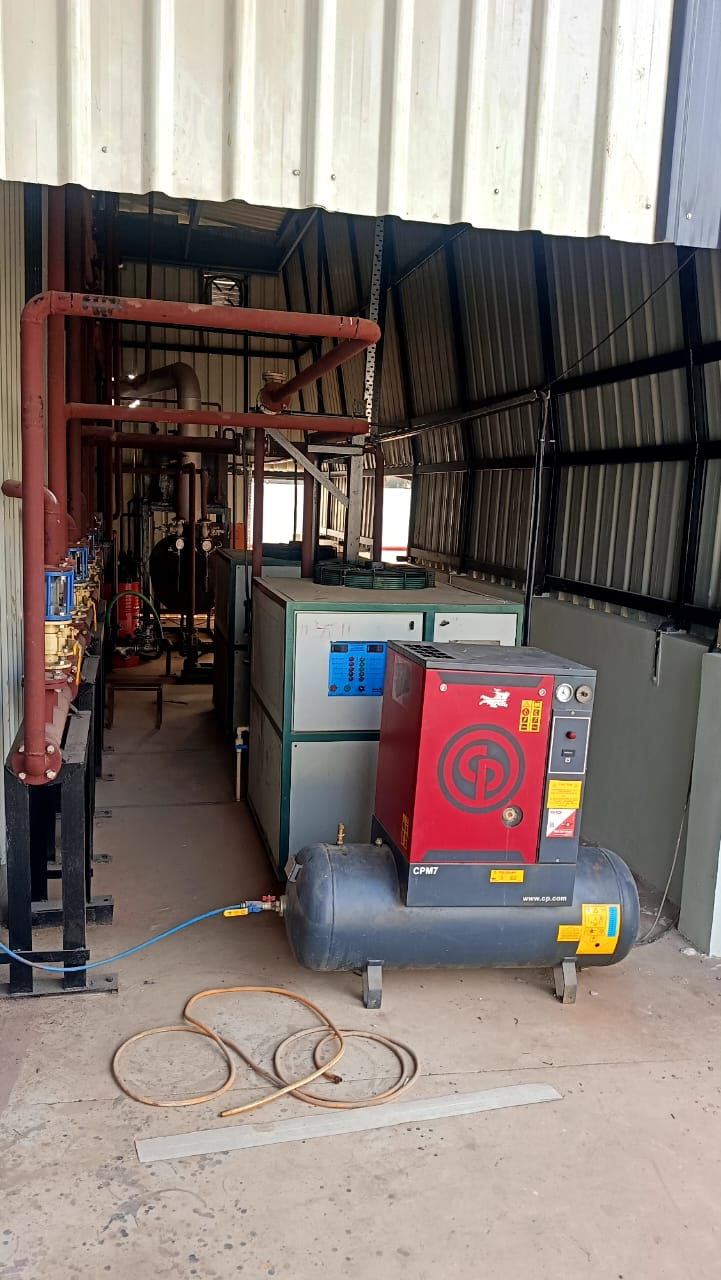
Dedicated compressed air station for automated valve actuation.
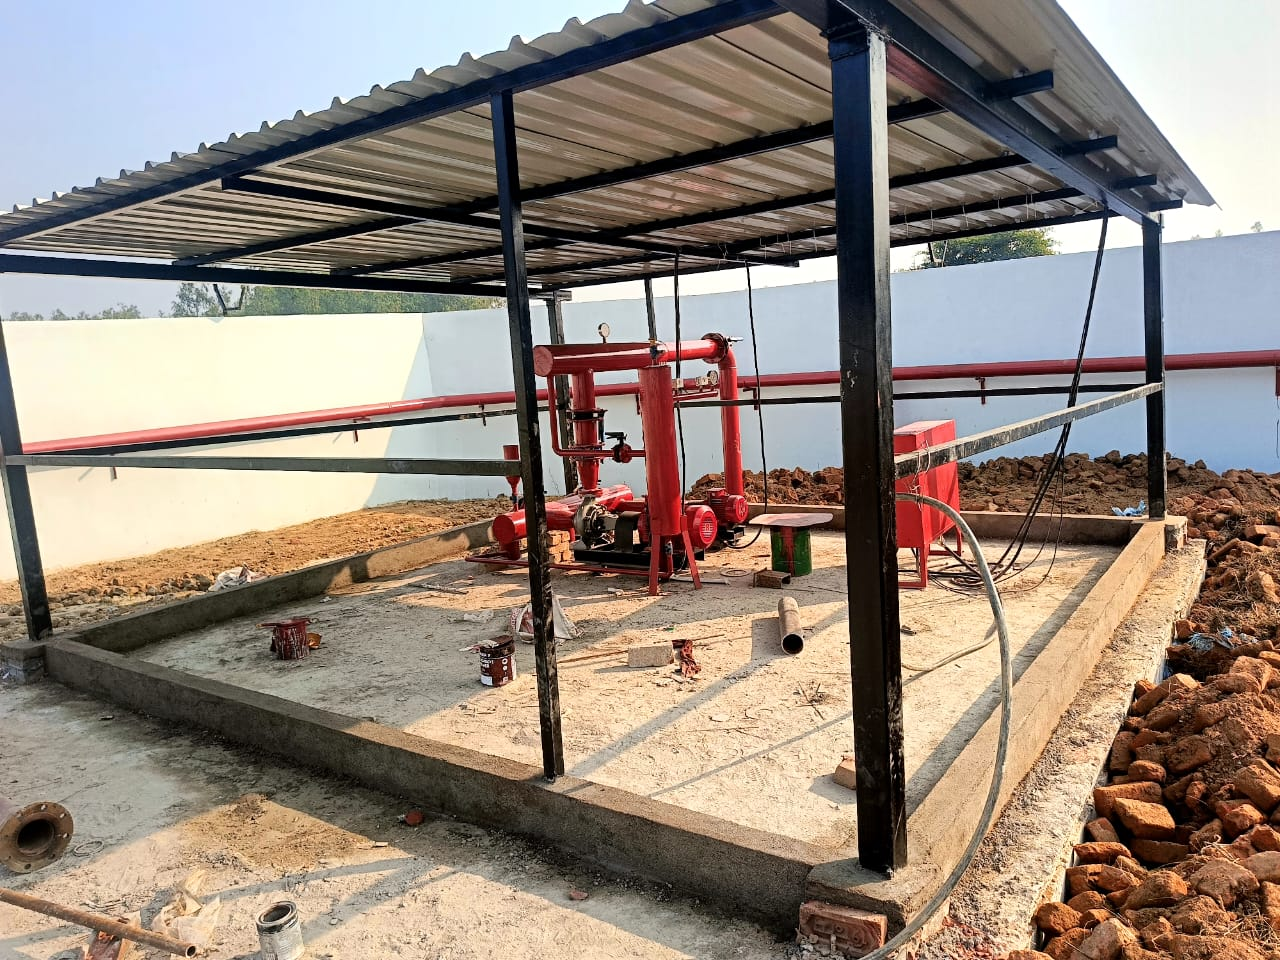
Industrial fire safety pumping assembly & perimeter hydrant header.
Acid value titration, FFA profiling, and batch sample retention.
Closed-cup flash point & gravimetric analytical verification.
Complete pre-dispatch BIS IS 15607:2022 analytical suite.
Engineered to meet stringent Indian petroleum blending specifications and downstream oleochemical industry standards.
High-cetane, ultra-low sulfur renewable diesel fuel (FAME) refined from UCO, Non-Edible Oils and Fats for direct OMC blending and institutional diesel fleets.
High-recovery natural glycerin co-product generated during modular batch transesterification, supplying downstream chemical, pharmaceutical, and industrial refining sectors.
Recovered high-FFA lipid fractions utilized across oleochemical synthesis, industrial soap and detergent manufacturing, lubricants, and rubber compounding.
Electronic 60-tonne weighbridge verification and FFA sampling of incoming UCO, non-edible oils, and fats into the 450 KL tank farm.
Particulate filtration, moisture removal, and thermal conditioning prior to catalytic batch dosing.
Targeted conversion of Free Fatty Acids (FFA) into methyl esters to prevent soap formation.
PLC-controlled modular batch reaction yielding FAME biodiesel and gravity-separated crude glycerol.
Distillation rectification towers recovering excess methanol for closed-loop reuse in subsequent batches.
Sub-atmospheric flash drying reducing moisture content well below the 500 mg/kg BIS limit.
Waterless ion-exchange resin beds followed by high-speed centrifuge filtration for crystal-clear B100.
Pre-dispatch BIS IS 15607:2022 batch approval in our Wet Chemistry Lab and calibrated OMC tanker loading.
Reach out for OMC supply coordination, UCO & non-edible feedstock partnerships, or oleochemical co-product inquiries.
Vill.- Bharawan, Sandila, Hardoi, Uttar Pradesh, India
Monday to Saturday • 9:00 AM – 6:30 PM
Complete the form below and our commercial or feedstock procurement desk will respond via email.